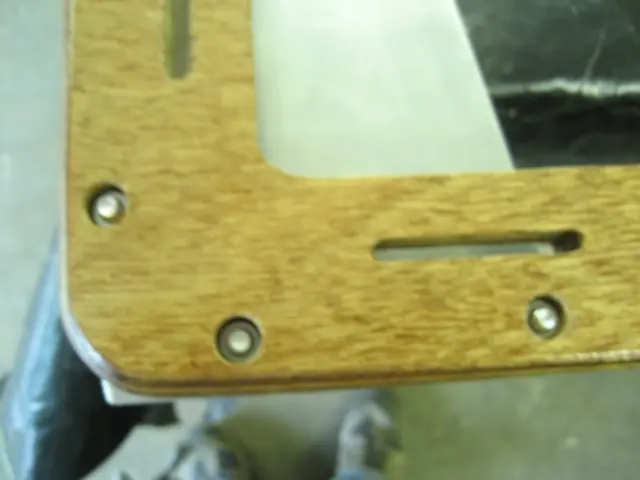
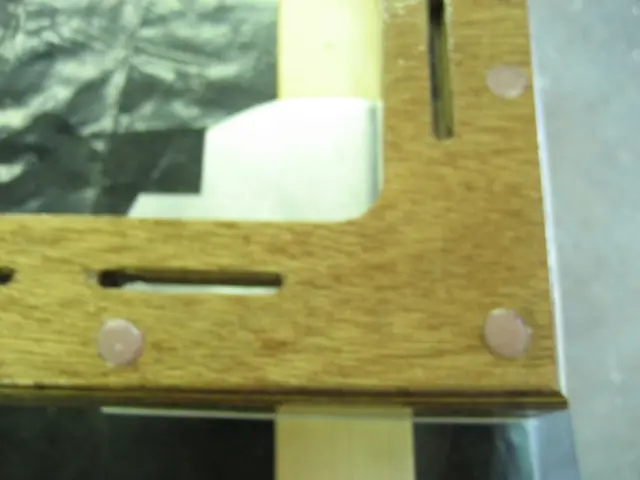
Seats: 1/4" diameter holes were drilled through the 7 layers of plywood to retain the aluminum se
1. 1/4" diameter holes were drilled through the 7 layers of plywood to retain the aluminum seat mounting plates. 1/4"-20 stainless steel nuts were set into 1/2" counter-bore holes.
2. To prevent the bolts from bonding to the epoxy, the nuts were drawn down with lightly-greased bolts and capped with an epoxy mixture consisting of West resin and 403 / 407 fillers.
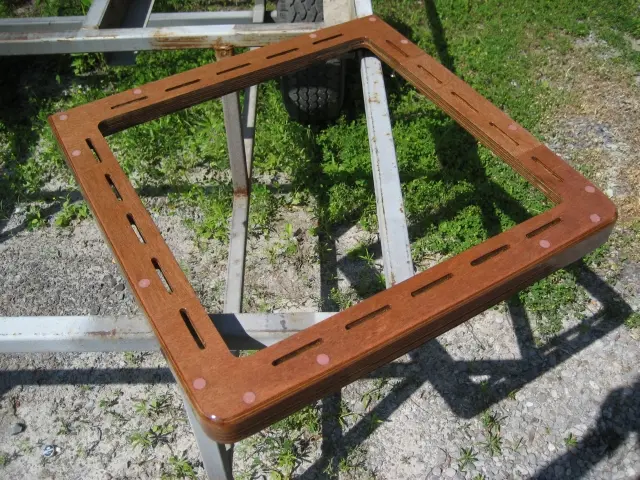
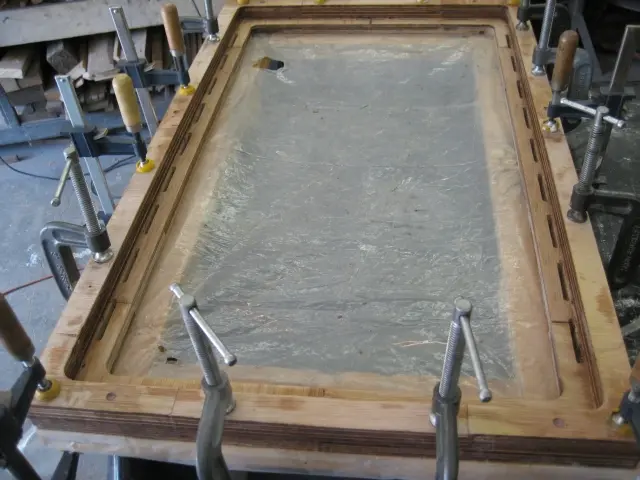
3. A passenger seat base was laminated over a buck built from scrap 1"x6" stock. Dimensions are 22" wide by 36" long.
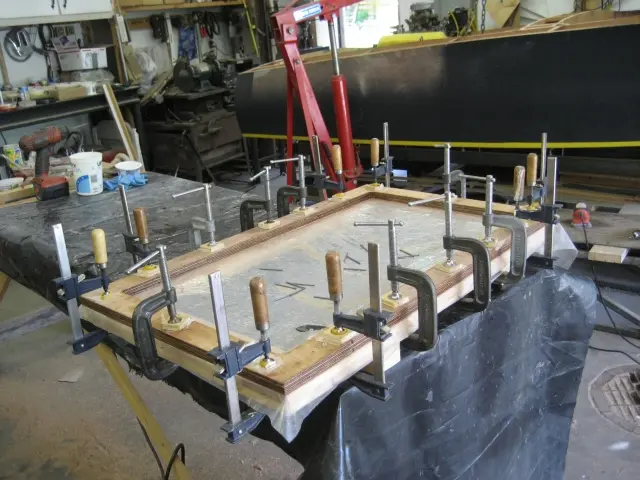
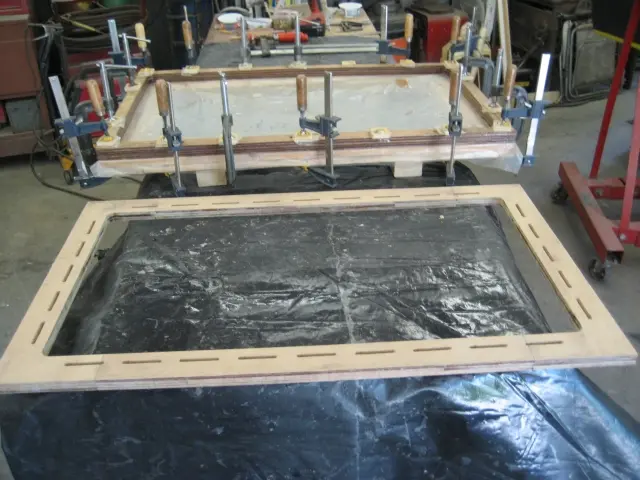
Seats: At the bottom of the photo, we see the passenger side seat base after routing for webbing
1. At the bottom of the photo, we see the passenger side seat base after routing for webbing. At the top of the photo, we're laminating the bottom half of the seat base.
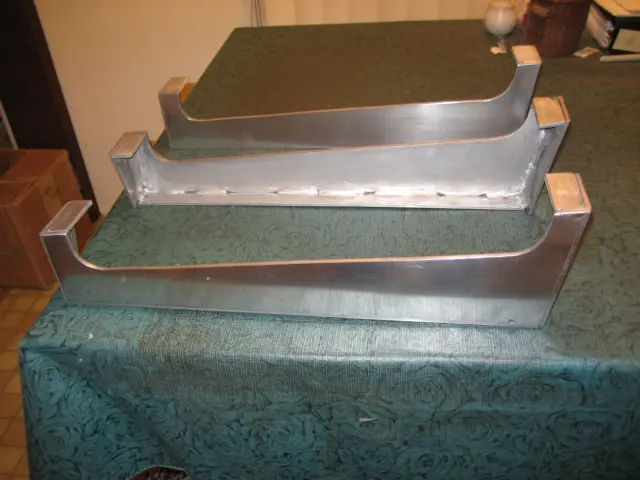
Seats: We could have built the passenger seat base supports from plywood, but aluminun will last
We could have built the passenger seat base supports from plywood, but aluminun will last forever. Our new horizontal metal bandsaw made quick work of cutting the 3/16" aluminum plate. Hope to install the seat base over the weekend.
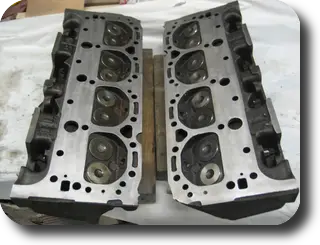
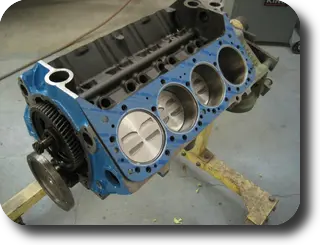
1. Rebuilt heads. New valves, valve guides and valve seats.
2. Marine head gasket.
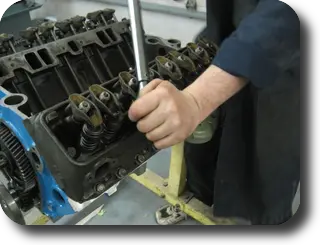
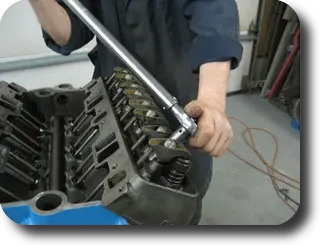
3. Cylinder heads torqued to 65 ft/lbs.
4. We completed the valve train by replacing the old solid lifters with a Comp Cams solid lifter kit. The original pushrods and rocker arms were in good shape so they were cleaned and reused.
1234
Nobody else here is logging a Hot Rod yet.
See the boat.